Engineering excellence in pharmaceutical formulation, clinical research, and ethical healthcare supply since inception.
Established as a progressive pharmaceutical formulation company, Forio Pharmaceuticals has grown into a premier hub for high-purity therapeutic solutions. Operating out of state-of-the-art facilities compliant with WHO-GMP, ISO 9001:2015, and DCGI guidelines, we manufacture and market a broad spectrum of medical formulations.
From basic antibiotic tablets to complex sustained-release capsules, sterile injectables, dry syrups, and nutraceutical supplements, our integrated chemical R&D and QA testing systems guarantee batch uniformity, bioavailability, and extended shelf life.
Guiding principles shaping our therapeutic innovations and business relationships.
To develop, manufacture, and distribute high-purity, bioavailable, and affordable medications across global markets while providing our PCD partners and contract clients with unmatched support.
To be globally recognized as a benchmark pharmaceutical manufacturer, pioneer advanced formulation technology, and expand healthcare accessibility across emerging and developed nations.
Uncompromising integrity in clinical research, absolute transparency in partner operations, continuous scientific innovation, and commitment to environmental safety standards.
High-speed rotary presses, automatic capsule fillers & ampoule sealers.
Class 100,000 cleanrooms preventing airborne contamination.
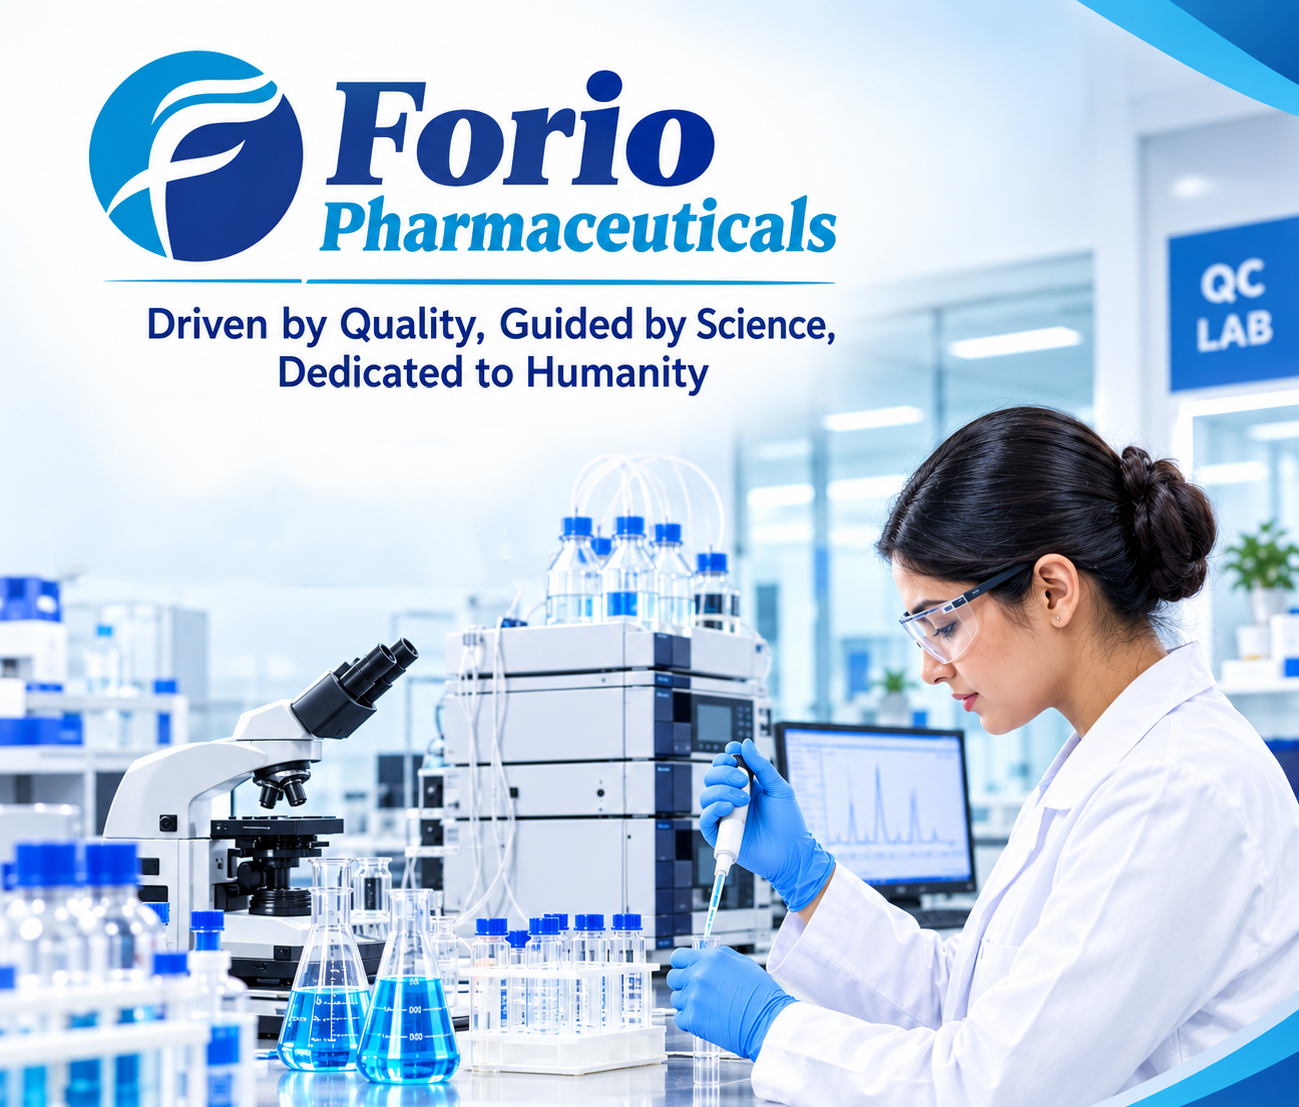
HPLC, UV Spectroscopy, dissolution apparatus & stability chambers.
Moisture and light barrier packaging for long chemical stability.
Our state-of-the-art production complex is engineered to satisfy global regulatory expectations. By strictly isolating production lines for beta-lactams, non-beta lactams, injectables, and nutraceuticals, we eliminate cross-contamination risks entirely.
Our leadership team brings decades of cumulative experience in pharmaceutical formulation, QA/QC, regulatory affairs, and supply chain management.
Formulation & Analytical Development
Dedicated scientists ensuring optimal pharmacokinetic properties, fast dissolution rates, and high stability for all tablet and capsule ranges.
Compliance & Regulatory Documentation
Certified QA managers tasked with raw material validation, batch release approvals, and maintaining international cGMP standards.
Partner Growth & Distribution
Managing nationwide PCD network logistics, promotional material dispatch, and priority order fulfillment for Third-Party clients.